

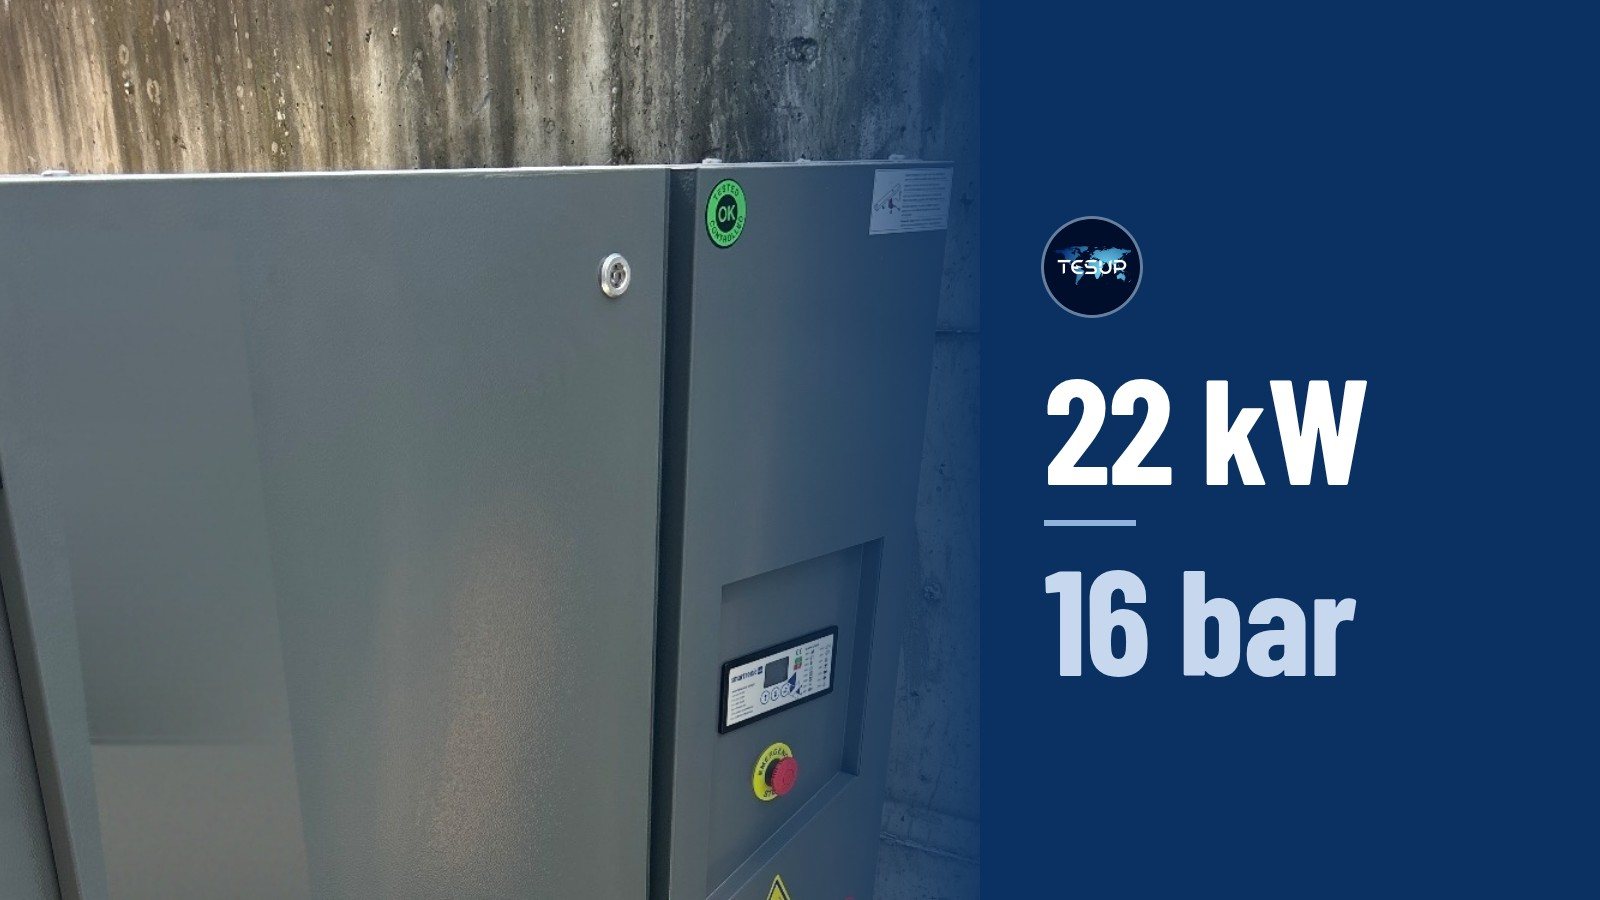
Seven machines were delivered to our production site this week. Not one of them cuts anything. They are the reason the machines that do cut can keep going, and they are the half of a factory that never makes it into a photograph.
A cutting hall runs on air.
It is easy to picture a factory as the machines that make the sparks. In practice, a cutting hall is a compressed air system with cutting machines attached to it. Air drives the pneumatics on every machine on the floor. It clamps and releases work. It clears a bed between jobs. Lose it and the impressive machines stand still, however new they are.
So when we add capacity to cut more aluminium, this is a large part of what we are actually buying: compressors, a dryer, a receiver, and the pipework to join them together.
Capacity is not the cutter. Capacity is the cutter, plus everything that has to be true for it to run all day.
Sixteen bar, not eight.
The compressor at the centre of this delivery is a 22 kW machine rated to sixteen bar. Ordinary workshop air runs at seven or eight. That gap is the whole reason it is here: the pressure is specified for what it feeds, not for the convenience of the pipework.
Higher pressure also means everything downstream has to be built to match. The dryer, the receiver, the fittings and the hose all carry the same rating, which is why a delivery like this arrives as a set rather than as one machine. It is a decision you make once, at the beginning, or pay for repeatedly afterwards.
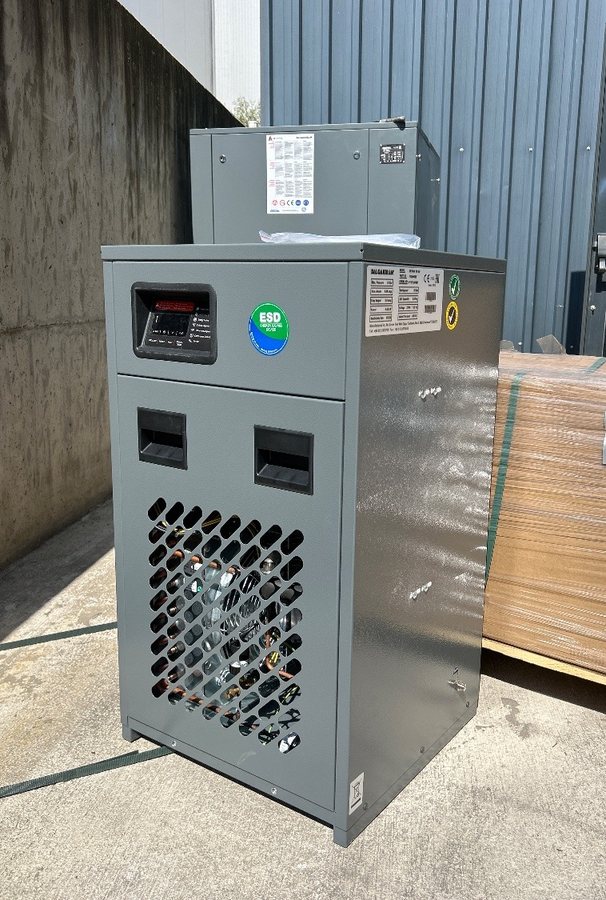
The dryer is the one that matters most.
Compress air and you concentrate the water that was already in it. That water then condenses somewhere downstream — in a line, in a valve, on a part. It corrodes pipework from the inside, it shortens the life of every pneumatic component it reaches, and on aluminium it leaves marks on surfaces we are about to coat.
A refrigerated dryer solves it in the least glamorous way possible: chill the air, let the moisture condense where you want it to, drain it away, and send the air on dry. Nobody photographs a dryer. It is still the single component that decides whether the rest of the system stays healthy.
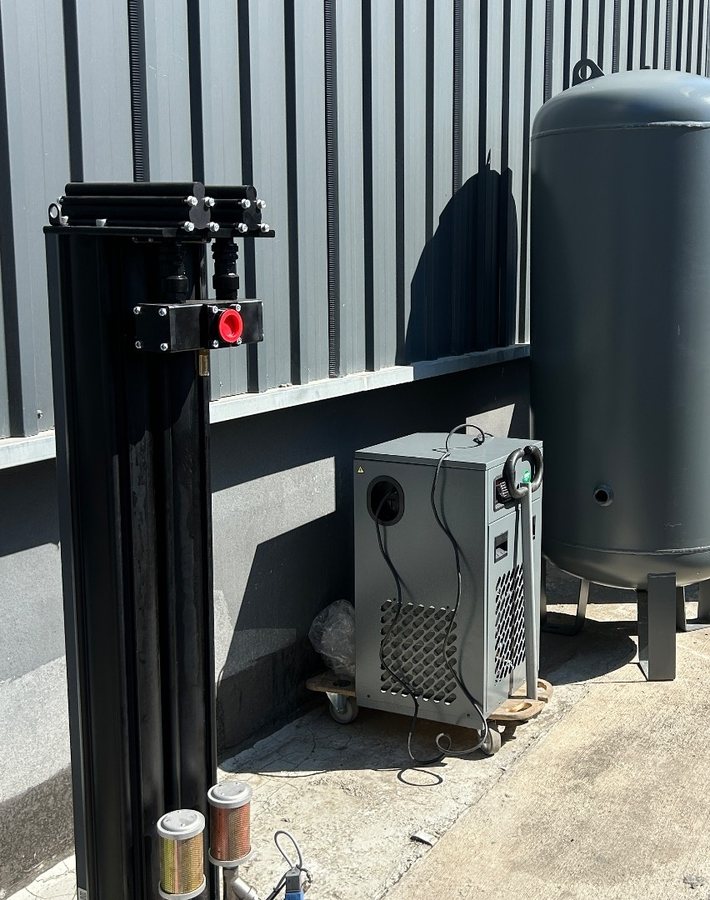
And the tank buys time.
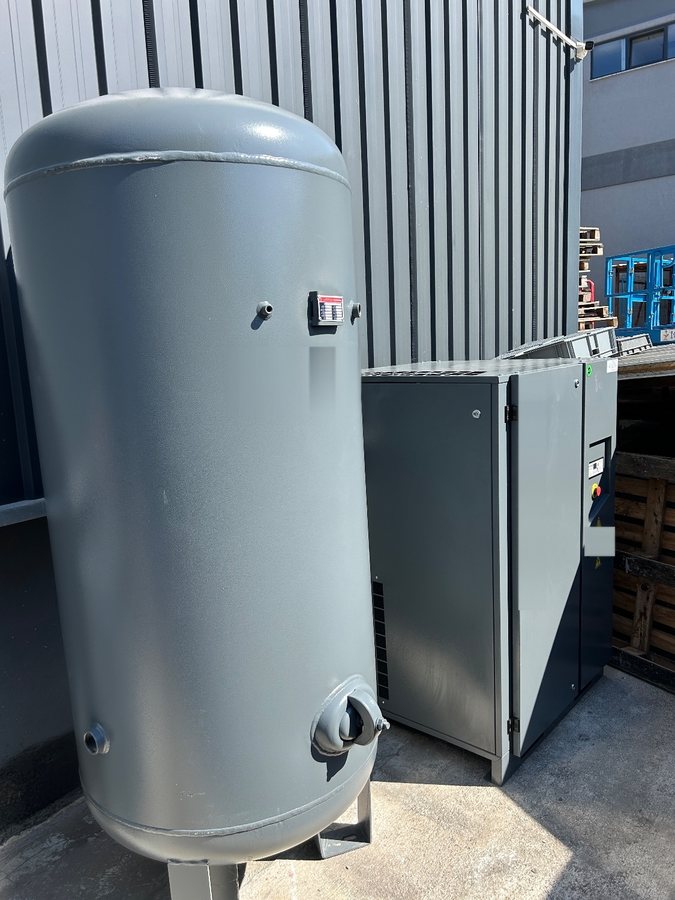
Demand in a workshop is not smooth. It arrives in bursts, and a compressor answering every burst on its own spends its life starting and stopping. The receiver absorbs that. It holds a reserve, flattens the peaks, keeps pressure steady at the far end of the hall, and lets the compressors run in a way that does not wear them out.
Steady pressure is not a comfort. It is the difference between a machine that behaves the same at four in the afternoon as it did at eight in the morning, and one that does not.
What this actually buys: hours.
None of this makes a cut faster. What it does is remove the reasons a cutting line stops: pressure sagging when three machines call at once, moisture reaching a valve, a single compressor carrying the whole building and having to be nursed.
More aluminium through the hall means more blades, more bodies, more covers. That output is limited by the hours the machines actually run, not by the number of machines on the floor. This delivery is about those hours.
Seven machines in.
None of them cuts.
All of them are why we can cut more.
The photographs on this page are our own, taken as the equipment was delivered and before any of it was installed.